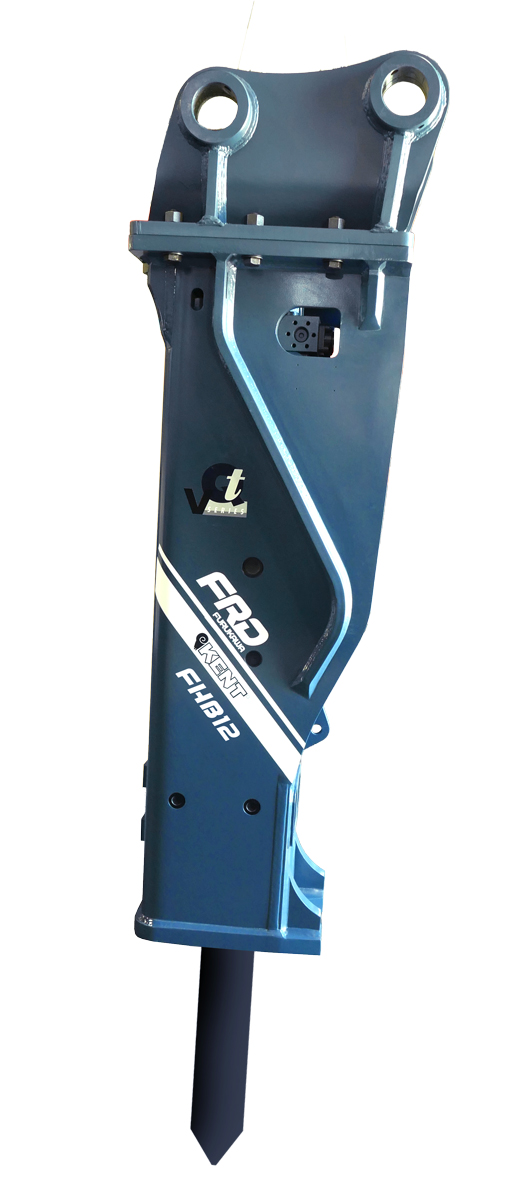
FHB12 Hydraulic Breaker for 9–15 Ton Excavators and Backhoes – SUPERIOR STRENGTH MEETS DURABILITY
FRD’s fifth-generation breaker, built without thru-bolts. The FHB12 rock breaker has a 9 to 15 ton carrier range making this mid-sized hammer the perfect choice for backhoes, excavators and mini-excavators.
The FRD FHB12 is a hydraulic breaker for excavators and backhoes in the 9 to 15 U.S. ton class, with 12 tons as the optimal carrier weight. It weighs 1,782 lb (810 kg), runs on 18.5 to 31.5 GPM at 2,320 to 2,610 psi, and delivers 450 to 670 blows per minute through 4.33 in (110 mm) working steel. It is the smallest model in FRD’s fifth-generation FHB Series and has a solid body with no thru-bolts.
PERFORMANCE SPOTLIGHT
What is new in the FHB12?
Like the other hammers in the FHB family, the FHB12 offers improved durability, with features that include a square, mono-block body for superior strength and a replaceable cylinder liner for reduced repair time.
Our unique design gives us an excellent power to weight ratio for lower maintenance and increased performance. This solid body concept eliminates thru-bolts which has reduced the breaker weight but does not affect our impact energy. This makes for much better control for the operator, less wear and tear on the excavator and reduced fuel costs.
The FHB12 ships in FRD’s Qtv cradle, a low-noise protective housing that accepts a wide range of top caps. The FHB Series builds on FRD’s Fx Series and adds updated stop pins and rod pins, a three-point dust intake prevention system, and a valve design that lowers hydraulic oil temperature.
Features & Benefits
- Enhanced internal hydraulics efficiencies leading to improved production
- Stop pins and rod pins updated to improve breaker durability
- Reduced CO2 emissions results in more eco-friendly operation.
- Eliminates thru-bolts.
- Increased hydraulic flow range for use on a wide carrier range.
- Mono-block design eliminates a separate cylinder, front-head and thru-bolts.
- Improved dust intake prevention system increases reliability.
- Replaceable cylinder liner with concentric porting keeps piston aligned for maximum impact performance.
- Improved valve design reduces hydraulic fluid temperatures, increasing performance.
- Square body design for superior strength.
- 3-point sealing system prevents internal contamination.
- Redesigned piston increases surface contact to working steel.
- TLB configuration suits rubber-tired backhoe applications.
- Qtv cradle for improved protection, sound suppression and dampening.
- Improved dampening system within the cradle keeps the breaker properly secure to reduce wear.
- Longer thrust bushing for increased internal alignment insures direct impact with piston.
- Includes two-year warranty with registration.
CARRIER COMPATIBILITY GUIDE for FHB12
Select Carrier Type